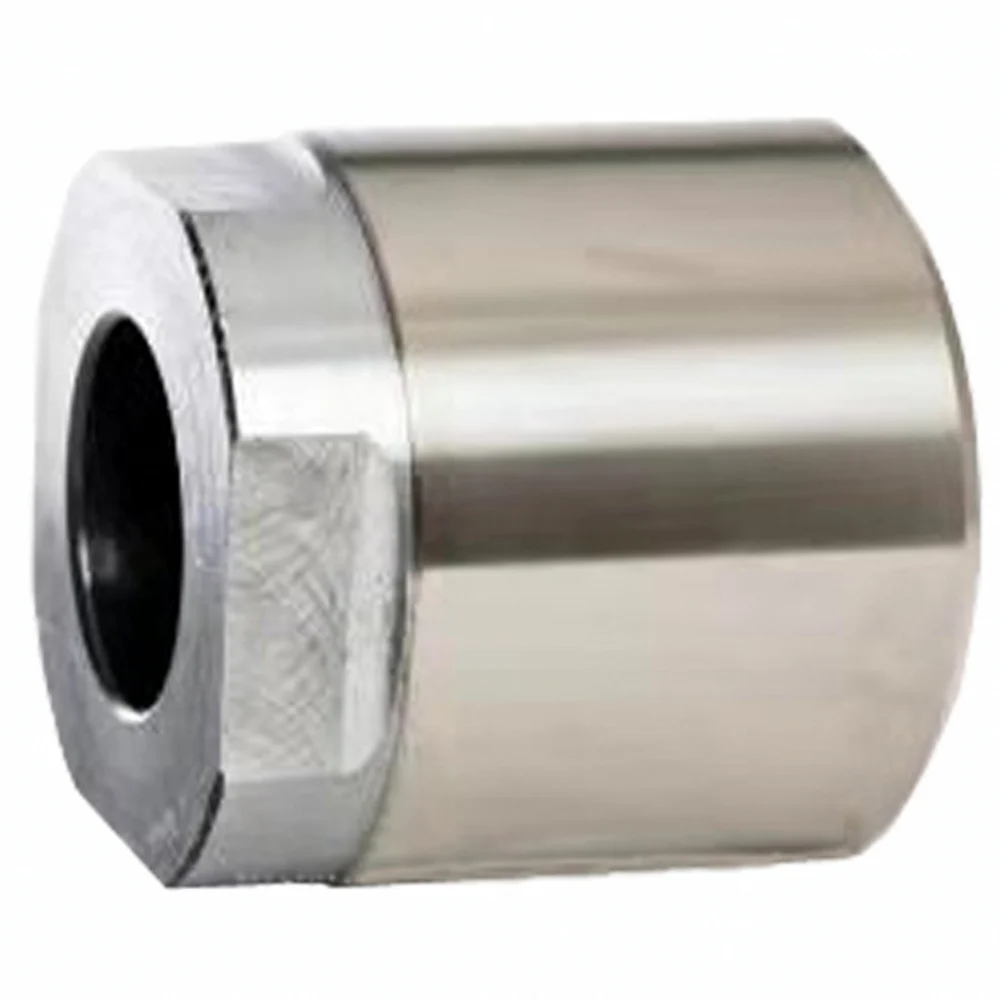
Review the head material or ring option, its listed diameter and the complete replacement interface together.
Die casting plunger tips for cold-chamber HPDC
The role of the plunger in die casting is to drive metal toward the die. In NADCA’s cold-chamber description, a plunger seals the sleeve’s inlet and pushes the introduced molten metal into the closed die. Keep the moving plunger assembly distinct from the sleeve it travels through.
A replacement request therefore needs to identify the head and its mating parts, rather than treating the names “plunger,” “tip” and “shot sleeve” as interchangeable order descriptions.
Four catalog plunger-head options
Nickel Alloy
Keep the required material specification with the Nickel Alloy plunger head replacement drawing.
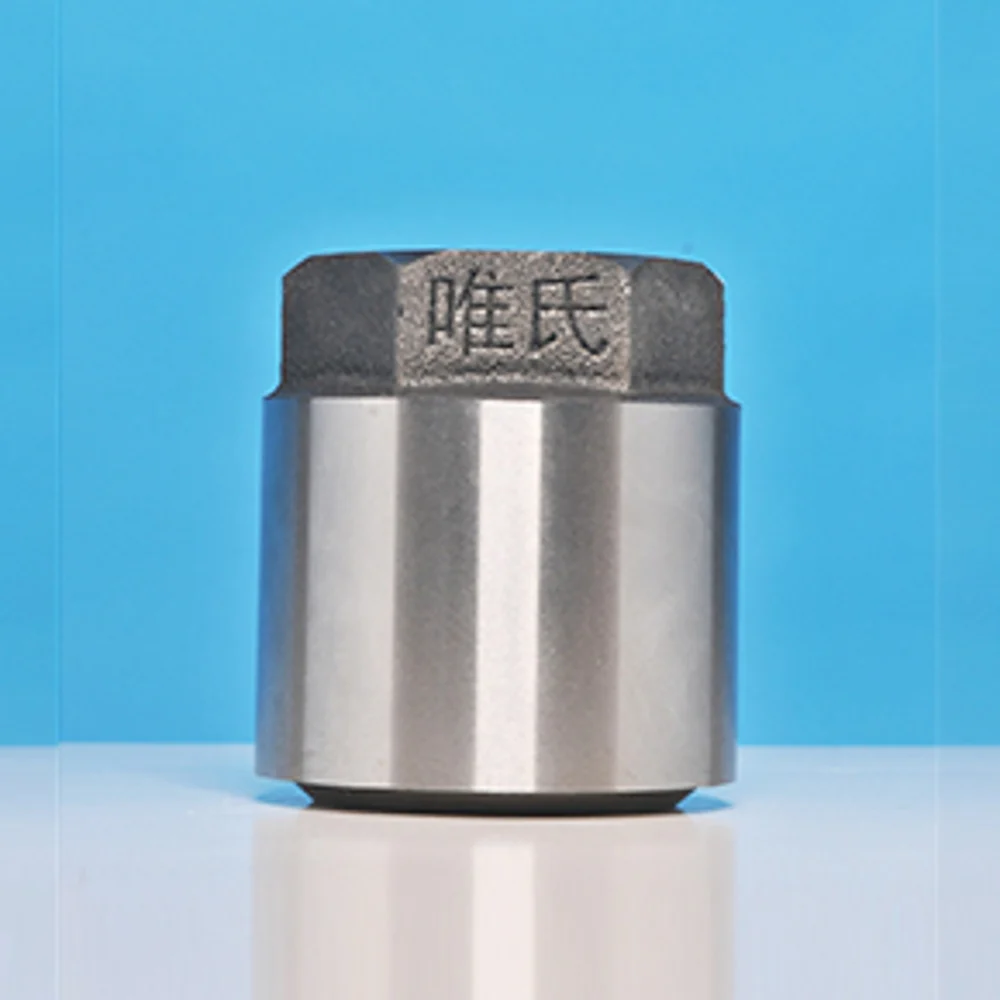
Nodular Cast Iron
For a Nodular Cast Iron head, match the existing material designation as well as its external form.
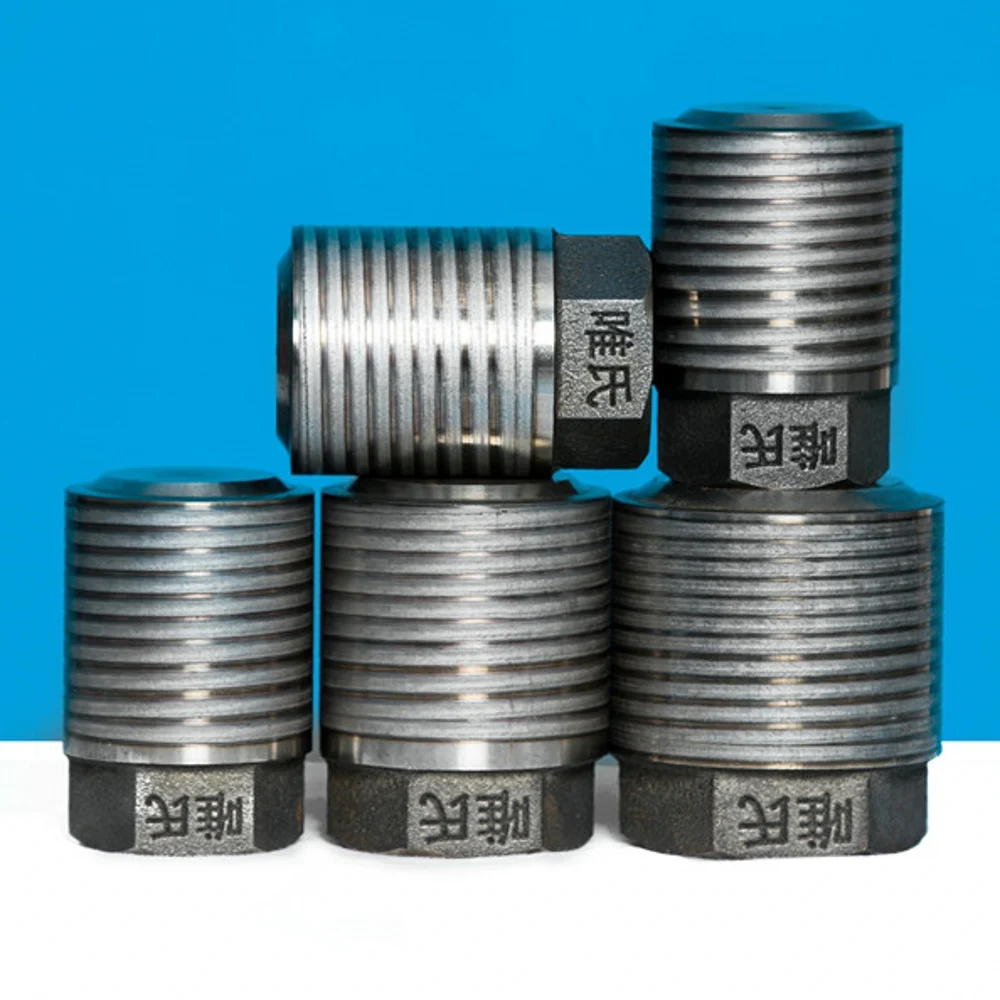
Nano Microcrystalline Laser
The Nano Microcrystalline Laser name is not a numerical wear, hardness or service-life guarantee. Specify required treatment and acceptance criteria separately.
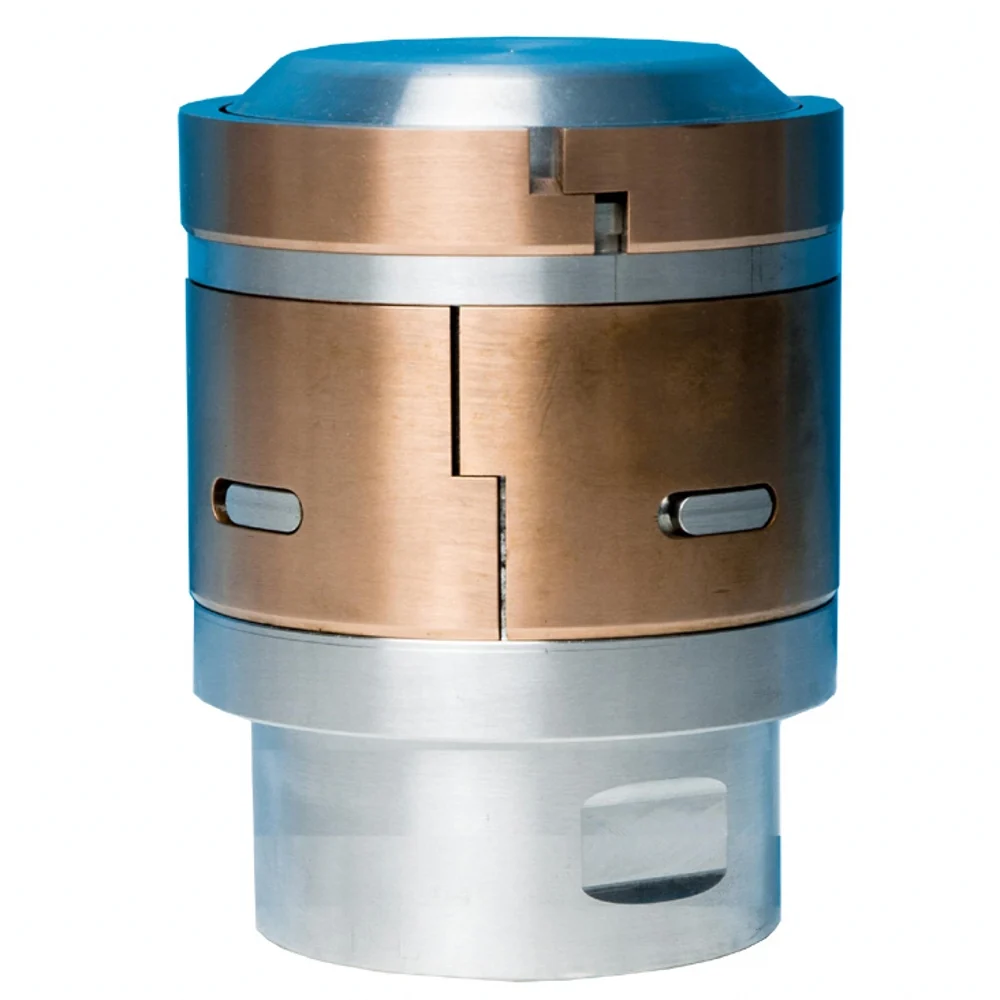
Combined Beryllium Copper Ring
Review the Combined Beryllium Copper Ring head with the ring configuration on the replacement drawing.
Standard and custom plunger-head diameters
| Catalogue list | Diameters, mm |
|---|---|
| Standard | 40, 50, 60, 70, 80, 90, 100, 110, 120, 130, 140, 150, 160, 170, 180, 190, 200 |
| Custom | 45, 55, 65, 75, 85, 95, 105, 115, 125, 135, 145, 155, 165, 175, 185, 195, 205 |
The same standard and custom lists appear in the four product descriptions. They are discrete listed sizes; the lists do not mean every possible intermediate diameter is a standard catalogue item.
Keep a catalogue diameter separate from the remaining fit details. A match in one dimension does not establish the head’s working length, attachment, ring arrangement or relationship with the existing sleeve.
Plunger tip for a die casting machine: interface review
For a replacement plunger tip for a die casting machine, provide one coordinated drawing or record covering:
- Head diameter and working length.
- Rod attachment and the specified thread or connection geometry.
- Front-face and ring arrangement.
- Cooling passages or connections, where required by the existing assembly.
- Machine identity, alloy and operating context.
Describe the existing arrangement first. Keep requested modifications distinguishable from a like-for-like replacement so the quotation answers the intended job.
Identify the actual head and related shot-end parts
The product images show different external forms, including smooth and grooved bodies and a ring assembly. Use the product name and drawing together; the photograph alone does not establish an exact replacement size.
Review die casting shot sleeves as the related component, and the chamber-process comparison for process context. Send the replacement information to sales@hotchamberdiecasting.com.
Questions and answers
Are these for hot-chamber or cold-chamber die casting?
The product descriptions identify these heads for cold-chamber high-pressure die casting machines. Keep that process designation in a replacement request; the component name alone does not establish compatibility with a hot-chamber machine.
Does Combined Beryllium Copper Ring mean a whole BeCu tip?
The full catalogue name identifies the combined ring option. Keep the head and ring construction explicit in the specification; that designation does not define an entire solid beryllium-copper head.
Does a matching diameter guarantee a replacement fit?
No. Diameter is one dimension. The attachment, working length, face and ring arrangement, and any required cooling interfaces also belong in the fit review. A complete assembly drawing is more useful than a diameter-only order description.